Loading product details
Preparing specifications, features and applications…
The V-65 Diaphragm Vacuum Pump delivers the highest flow rate in the compact V Series range at 65 L/min — specifically designed for demanding laboratory conditions where higher vacuum system throughput, faster evacuation of larger connected systems, or multiple simultaneous vacuum connections require flow capacity beyond the V-40's 35 L/min. Maintaining the V Series' comprehensive chemical resistance through PTFE pump head, PTFE composite diaphragm, and FPM valve construction — the V-65 achieves 8 mbar ultimate vacuum at 400W with a 12 mm interface specification that reduces pressure drop at the pump inlet for high-flow applications. The V-65's direct drive system, quiet low-vibration performance, and continuous operation rating make it the appropriate choice for pharmaceutical process vacuum, high-throughput chemical laboratory filtration, and demanding corrosive gas environments requiring reliable high-capacity oil-free vacuum. Enquire today.
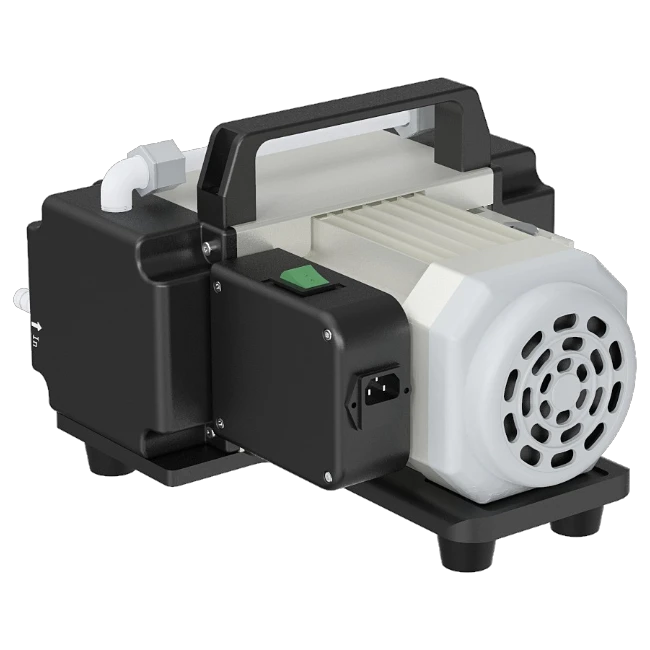
The V-65 Diaphragm Vacuum Pump delivers the highest flow capacity in the compact V Series at 65 L/min — combining PTFE pump head, PTFE composite diaphragm, FPM valves, 12mm low-pressure-drop interface, oil-free direct drive, and continuous duty rating for high-capacity pharmaceutical, chemical, and corrosive environment laboratory vacuum applications.
The V-65's 65 L/min maximum flow — nearly double the V-40's 35 L/min — enables faster initial evacuation of larger vacuum systems, supports simultaneous high-flow vacuum supply to multiple connected processes, and maintains stable vacuum during high-vapour-generation processes such as active large-scale solvent evaporation and continuous high-throughput filtration. The high-flow design is achieved through optimised pump head geometry and direct drive motor specification at 400W — providing the mechanical power required for reliable 65 L/min pumping against the full 8 mbar to 1 bar operating pressure range.
The V-65's PTFE composite diaphragm processes the largest volume of corrosive laboratory vapour per unit time of any model in the compact V Series — making the PTFE material's long-term chemical resistance to acid vapours, halogenated solvents, and reactive gas streams proportionally more important for service life and consistent performance. In demanding pharmaceutical and chemical laboratory environments where the V-65 may process corrosive vapours continuously throughout the working day, PTFE's near-universal chemical inertness provides the operational reliability that standard rubber or silicone diaphragm materials cannot deliver under sustained corrosive gas exposure.
The V-65 provides 65 L/min of clean, oil-free vacuum — free from the hydrocarbon mist contamination that would otherwise be carried into the vacuum system at proportionally higher volumes by an equivalent-flow oil-sealed rotary vane pump. At 65 L/min flow rate, the oil mist issue of a conventional rotary vane pump would be substantially more problematic than at lower flow rates — more oil mist per unit time reaching connected analytical instruments and process equipment. The V-65's oil-free design eliminates this risk at the higher flow scale.
Despite its higher 400W operating power, the V-65 maintains the V Series' characteristic low-vibration and quiet operation — achieved through direct drive diaphragm mechanism design optimisation appropriate for the higher pumping capacity. Low vibration at 65 L/min is a more demanding engineering requirement than at 20 L/min — the V-65's mechanism design addresses this to maintain laboratory-compatible acoustic and mechanical performance standards across the higher flow capacity.
The V-65's direct electric drive system connects motor output directly to the diaphragm mechanism at 400W — providing reliable, consistent 65 L/min performance throughout the continuous operating cycle without belt-related performance degradation. In demanding pharmaceutical and chemical laboratory environments where the V-65 operates under sustained high-flow conditions throughout the working day, the direct drive system's absence of mechanical transmission wear components ensures consistent vacuum performance without the progressive flow rate decline associated with belt wear in indirect drive diaphragm pumps.
The V-65 uses a 12 mm interface specification — compared to the 10 mm interface of the V-20 and V-40 — providing larger-bore inlet connections that reduce pressure drop at the pump inlet during high-flow operation. At 65 L/min, the pressure drop through the inlet connection is proportionally greater than at 20 or 35 L/min, and maintaining a low-resistance inlet path through the wider 12 mm interface directly supports the pump's ability to achieve its rated flow rate and ultimate vacuum in connected systems. The 12 mm interface is compatible with standard laboratory vacuum tubing in the appropriate bore size.
The V-65 Diaphragm Vacuum Pump incorporates overheat protection, stable vacuum operation, and reliable motor safety — providing safe, high-capacity continuous vacuum for demanding pharmaceutical, chemical, and corrosive gas laboratory applications.
The V-65's overheat protection system automatically shuts down the 400W motor if operating temperature exceeds the safe limit — critical for a high-power pump expected to operate continuously in warm laboratory environments under demanding high-flow conditions. At 400W, the V-65 generates significantly more heat than smaller V Series models — making adequate ventilation clearance around the pump and functional overheat protection essential requirements for reliable continuous operation in pharmaceutical and chemical laboratory environments.
The V-65's two-stage PTFE pump head delivers stable, consistent 65 L/min vacuum output throughout the continuous operating cycle — preventing the vacuum fluctuations that would disrupt high-throughput filtration, active large-scale rotary evaporation, and continuous pharmaceutical process vacuum during demanding extended operation sessions. Stable high-flow vacuum is the primary operational requirement for the pharmaceutical process and high-capacity chemical laboratory applications that define the V-65's use context.
The V-65's 400W motor is designed for safe, reliable continuous operation within the specified ambient conditions — with motor insulation, winding specifications, and thermal management appropriate for the highest-power continuous duty cycle in the compact V Series range. The reliable motor safety design protects against electrical faults and thermal failures that would cause process interruption during critical high-throughput pharmaceutical and chemical laboratory vacuum operations.
Explore alternative models and related solutions from other categories