Loading product details
Preparing specifications, features and applications…
The VRD-16 Oil Rotary Vane Vacuum Pump is the high-performance model of the VRI/VRD Series — introducing four key performance and specification advances over the VRI models that position it as the industrial and demanding research laboratory vacuum pump of choice. First, 16 m³/h displacement for maximum-flow vacuum supply. Second, significantly improved 4×10⁻² Pa ultimate partial pressure — the deepest vacuum in the series. Third, fluororubber seals throughout for enhanced corrosion resistance against aggressive chemical vapours. Fourth, a double anti-return oil structure that prevents oil contamination more effectively than single-valve systems. Combined with an advanced exhaust valve for extended service life, KF25 inlet for lower pressure drop at high flow, single or three-phase power options, and a remarkably quiet ≤58 dB noise level — the VRD-16 is the definitive high-performance vacuum pump for industrial vacuum systems, research laboratory high-flow applications, chemical and pharmaceutical processing, and demanding vacuum oven service. Enquire today.
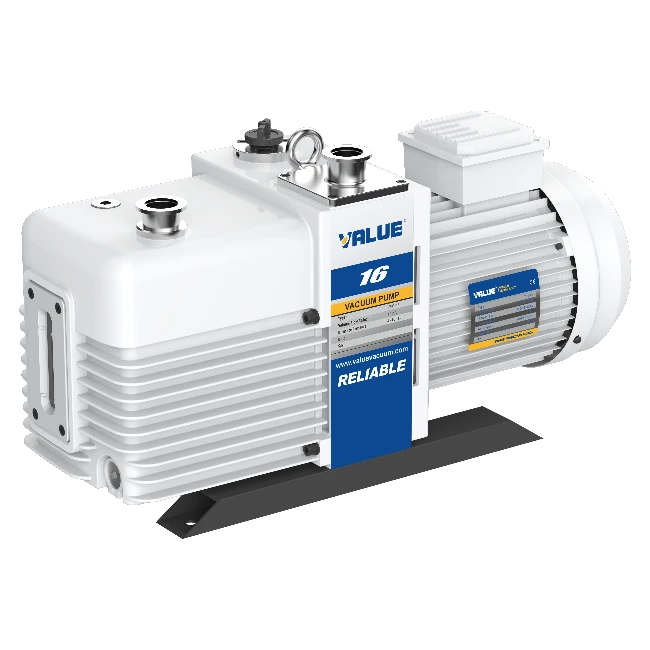
The VRD-16 delivers the highest performance in the VRI/VRD Series — two-stage 16 m³/h vacuum at 4×10⁻² Pa ultimate partial pressure with fluororubber seals for chemical resistance, double anti-return oil structure, advanced exhaust valve, KF25 low-drop inlet, single/three-phase flexibility, ≤58 dB quiet operation, and integrated pump body for industrial vacuum systems, research laboratories, and demanding chemical and pharmaceutical vacuum applications.
The VRD-16's two-stage rotary vane mechanism achieves 4×10⁻² Pa ultimate partial pressure — more than twice as deep as the VRI series' 1×10⁻¹ Pa — through an optimised two-stage compression architecture that routes gas through two stages with improved inter-stage efficiency. This deeper ultimate vacuum enables the VRD-16 to support applications requiring sub-millipascal vacuum levels — including molecular distillation, high vacuum system backing, electron beam instrument foreline support, and high-precision analytical instrument vacuum supply — that the VRI series cannot reliably serve.
The VRD-16's fluororubber (FKM/Viton) seals provide substantially superior chemical resistance compared to the standard nitrile or EPDM seals used in basic rotary vane pump designs — resisting aggressive organic solvents (chlorinated solvents, aromatic compounds, ketones), acidic vapours (HCl, HNO₃, acetic acid), and reactive gases encountered in demanding chemical synthesis and pharmaceutical manufacturing vacuum applications. The fluororubber seals maintain their elasticity and sealing contact in the aggressive chemical environments that rapidly degrade standard rubber seals — extending the VRD-16's service life in chemically demanding applications and reducing the frequency of seal replacement maintenance.
The VRD-16's double anti-return oil structure provides two independent barriers preventing oil backflow into the connected vacuum system during pump shutdown and power failure — a more robust anti-contamination architecture than the single solenoid valve of the VRI series. The double structure ensures that even if one anti-return mechanism is compromised by wear or partial failure, the second provides continued protection — critical for pharmaceutical and high-value analytical applications where oil contamination is unacceptable.
The VRD-16's advanced exhaust valve design maintains reliable high-cycle opening and closing performance across extended service — using materials and geometry optimised for the higher flow rates and pressures of 16 m³/h two-stage operation. The long-service-life exhaust valve reduces maintenance intervals compared to standard designs, contributing to the VRD-16's suitability for demanding industrial continuous-duty vacuum service where frequent maintenance interruptions reduce production efficiency.
The VRD-16's KF25 (NW25 nominal bore) inlet provides 56% more cross-sectional area than the KF16 inlet of the VRI series — substantially reducing the pressure drop at the pump inlet during 16 m³/h high-flow operation. At high flow rates, inlet pressure drop becomes a meaningful performance limitation if the bore is undersized — the KF25 inlet ensures that the VRD-16's rated 16 m³/h flow and 4×10⁻² Pa ultimate pressure are achieved in actual connected systems rather than being limited by inlet restriction.
The VRD-16 is available in single-phase (for standard laboratory circuits) and three-phase power configurations — providing installation flexibility for industrial facilities where three-phase electrical infrastructure is the standard for high-power industrial equipment. Three-phase operation provides more balanced motor loading, smoother torque delivery at 16 m³/h operating speeds, and improved efficiency compared to single-phase at the same 0.55 kW rating — making three-phase the preferred option in industrial settings with three-phase supply availability.
The VRD-16's ≤58 dB noise level is the quietest in the VRI/VRD Series — quieter than both the VRI-4 (≤62 dB) and VRI-8 (≤65 dB) despite its significantly higher 16 m³/h flow capacity. This counter-intuitive performance is achieved through the VRD-16's optimised integrated pump body structure, balanced rotor design, and advanced exhaust valve system that collectively reduce mechanical noise generation more effectively than the simpler VRI series designs.
The VRD-16's integrated monolithic pump body structure provides superior rigidity and dimensional stability compared to multi-piece assemblies — maintaining precise rotor-to-stator clearances throughout the pump's operating life and in the vibration environments of industrial installations. High-quality materials throughout the pump mechanism contribute to the long service life and consistent performance that industrial continuous-duty vacuum applications demand.
The VRD-16 incorporates a double anti-return oil structure for comprehensive contamination prevention, stable vacuum system operation, and reliable motor and thermal protection — providing the highest level of vacuum system safety in the VRI/VRD Series for industrial and demanding research laboratory applications.
The double anti-return oil structure provides two independent barriers against oil backflow — ensuring that connected industrial process equipment, analytical instruments, and pharmaceutical vacuum systems are protected against oil contamination during pump shutdown, power interruption, and maintenance events. The redundant double-barrier design provides substantially higher reliability of contamination prevention than single-valve systems.
The VRD-16's two-stage mechanism, fluororubber seals, and advanced exhaust valve system collectively provide stable vacuum maintenance at 16 m³/h under the demanding gas loads of industrial continuous-duty vacuum operation — preventing the pressure fluctuations that disrupt industrial process quality and analytical measurement validity.
The VRD-16's 0.55 kW motor (single or three-phase) incorporates thermal protection against overload and sustained high-temperature operation — safeguarding the motor during intensive continuous industrial vacuum duty cycles and providing automatic shutdown before thermal damage occurs.
Explore alternative models and related solutions from other categories