Loading product details
Preparing specifications, features and applications…
The VRI-8 Oil Rotary Vane Vacuum Pump doubles the flow capacity of the compact VRI-4 — delivering 8 m³/h dual-stage rotary vane vacuum pumping for laboratory and industrial vacuum applications requiring faster chamber evacuation, higher sustained gas load handling, or simultaneous vacuum supply to multiple connected systems. Maintaining the VRI-4's core feature set of dual-stage architecture, built-in gear pump for steady oil supply, electric solenoid valve for oil backflow prevention, integrated pump-motor design, and IP44 environmental protection — the VRI-8 adds the higher 0.55 kW motor power and 0.5L oil capacity needed for the increased continuous duty demands of 8 m³/h operation. With 1×10⁻¹ Pa ultimate partial pressure, 3 Pa total pressure, KF16 connections, ≤65 dB noise, and 17 kg compact weight — the VRI-8 serves vacuum drying systems, pharmaceutical applications, chemical processing, and industrial vacuum processes requiring reliable higher-flow deep vacuum supply.
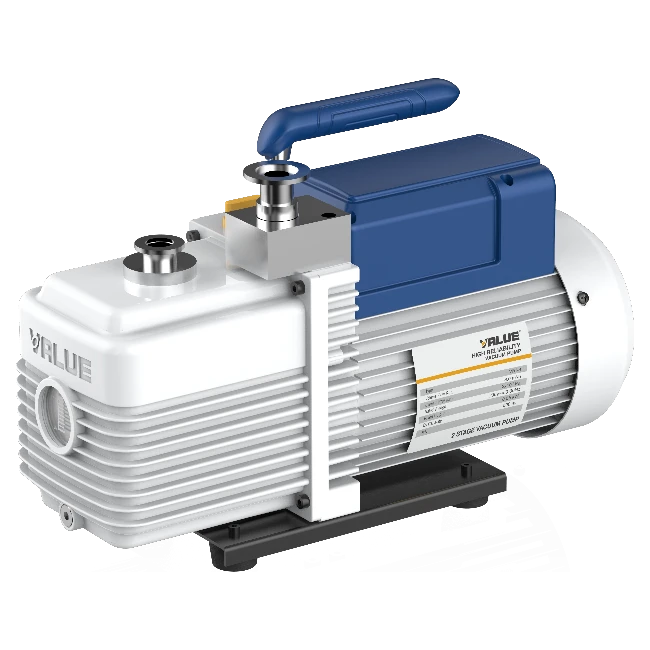
The VRI-8 delivers 8 m³/h dual-stage oil rotary vane vacuum with built-in gear pump for steady oil supply, electric solenoid anti-backflow valve, integrated pump-motor design, IP44 protection, and ≤65 dB operation — providing reliable higher-capacity deep vacuum supply for laboratory vacuum drying systems, pharmaceutical, chemical, and industrial vacuum process applications.
The VRI-8's dual-stage mechanism operates on the same series-compression architecture as the VRI-4 — routing gas through two sequential compression stages to achieve 1×10⁻¹ Pa ultimate partial pressure. At 8 m³/h, the VRI-8 processes twice the gas volume per unit time compared to the VRI-4 — evacuating larger vacuum chambers faster, maintaining deeper vacuum under higher sustained gas loads from active drying operations, and supporting simultaneous multiple instrument vacuum supply without the flow bottlenecking that limits the compact VRI-4 under multi-connection loads.
The VRI-8's built-in gear pump provides continuous pressurised oil delivery to the dual-stage rotary vane mechanism — ensuring uninterrupted lubrication and sealing at the higher operating speeds and sustained duty cycles of 8 m³/h continuous industrial and laboratory vacuum operation. The larger 0.5L oil capacity of the VRI-8 (vs 0.3L VRI-4) provides greater oil reserve for extended continuous operation between oil level checks, and the gear pump's positive displacement delivery maintains consistent oil flow even under the increased thermal and mechanical demands of higher-capacity continuous-duty operation.
The VRI-8's solenoid valve provides the same instant power-failure oil suck-back prevention as the VRI-4 — critical at the VRI-8's higher 8 m³/h capacity where the reverse flow energy during pump coast-down could draw a larger quantity of oil into the connected vacuum system than the compact VRI-4 would experience. The solenoid valve's instant closure on power interruption protects all connected vacuum ovens, drying systems, and process equipment from oil contamination regardless of the number of simultaneously connected instruments.
The VRI-8's oil-lubricated dual-stage mechanism provides long service life through continuous lubrication — with the 0.55 kW motor and dual-stage pump designed for sustained industrial and laboratory continuous-duty operation. The durable construction enables the VRI-8 to serve as a reliable central vacuum source for multi-instrument laboratory vacuum supply networks, industrial process vacuum systems, and pharmaceutical drying operations requiring consistent vacuum performance throughout extended continuous working periods.
The VRI-8's 395 × 145 × 257 mm compact format and 17 kg weight — modest increases over the VRI-4's dimensions — maintain bench-mountable practicality for a higher-capacity dual-stage oil vacuum pump. This compact efficiency makes the VRI-8 suitable for laboratory environments where the VRI-4's 4 m³/h is insufficient but a large industrial pump would occupy excessive bench or floor space.
Direct motor-to-pump coupling eliminates transmission losses and maintenance requirements — providing stable 8 m³/h performance at 1440 rpm without the progressive flow rate decline associated with belt wear in indirect drive systems. The integrated design maintains consistent vacuum performance throughout the VRI-8's service life without periodic belt tension adjustments.
The VRI-8 incorporates solenoid anti-backflow protection, stable vacuum retention, and motor protection — providing safe higher-capacity continuous laboratory and industrial vacuum operation.
The solenoid valve instantly closes at power interruption — preventing oil contamination of connected vacuum systems during pump shutdown at the VRI-8's higher 8 m³/h capacity, where coast-down reverse flow could deliver more oil to connected systems than the compact VRI-4 would generate.
Dual-stage compression and efficient oil sealing maintain consistent vacuum at connected vacuum systems — preventing pressure fluctuations during high-gas-load active drying and chemical processing operations at the VRI-8's higher flow capacity.
The VRI-8's 0.55 kW single-phase motor incorporates thermal protection against overload conditions — safeguarding the higher-power motor during the continuous high-duty cycles of industrial and laboratory vacuum supply operation.
Explore alternative models and related solutions from other categories