Loading product details
Preparing specifications, features and applications…
The RV-50A Rotary Evaporator is the flagship high-capacity unit of the RV Series — purpose-built for large-scale solvent evaporation, industrial chemical processing, pharmaceutical production support, and large-volume research operations where no smaller rotary evaporator format can meet the throughput and batch volume requirements. With a 50L rotary flask, 20L collection bottle, 9 L/h maximum evaporation rate, and a 1.75 m² condenser area — the largest in the RV Series — the RV-50A delivers production-adjacent processing capability backed by PID temperature precision (±1°C), 8 mbar ultimate vacuum, 5300W high-capacity heating, and an aluminum alloy bracket engineered for the structural demands of 50L-scale glassware and solvent loads. Contact us today to enquire about the RV-50A.
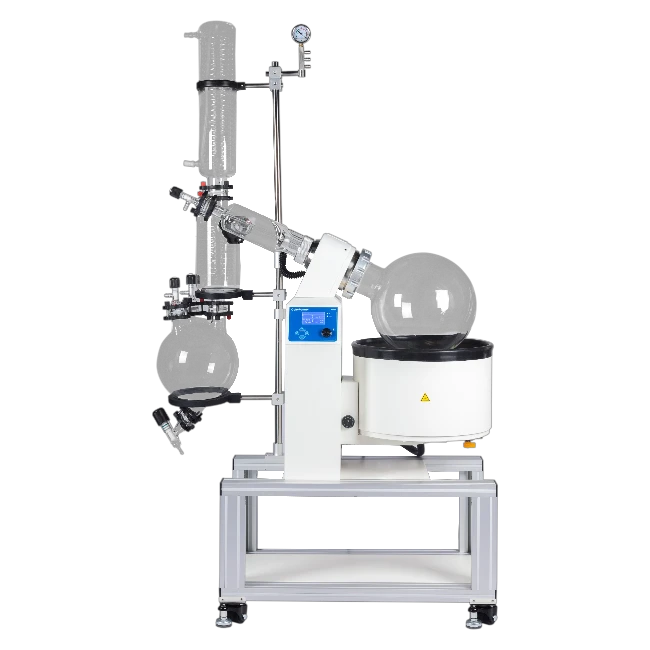
The RV-50A Rotary Evaporator leads the RV Series in every capacity and performance metric — delivering 50L batch processing, 9 L/h evaporation rate, 1.75 m² condenser, 5300W PID-controlled heating, and 280mm auto lift on a robust aluminum alloy frame, providing the processing power and structural strength required for industrial-scale and large-volume pharmaceutical solvent evaporation.
The RV-50A's 50L rotary flask is the largest in the RV Series — enabling processing of batch volumes that would require multiple sequential runs on a 20L system, dramatically reducing total processing time for large-scale solvent recovery operations. The paired 20L collection bottle provides the largest solvent recovery storage in the series, accommodating extended high-rate evaporation runs without requiring intermediate emptying. For industrial chemical laboratories, pharmaceutical production support facilities, and large-scale research operations, the 50L batch capacity defines a step-change in processing efficiency relative to pilot-scale equipment.
The RV-50A's rotation system drives the 50L flask assembly at speeds from 20 to 110 rpm — a range calibrated for the large-format, high-mass flask that requires lower rotational speeds than smaller formats to achieve optimal thin-film formation without excessive mechanical stress on the glassware or drive mechanism. The system maintains stable, vibration-free orbital motion across the full speed range, ensuring consistent thin-film formation across the entire inner surface of the 50L flask — maximising the effective evaporation area and heat transfer efficiency at production scale.
The RV-50A's LCD display provides continuous real-time monitoring of bath temperature, rotation speed, and operational status throughout the evaporation process. At 50L production scale, continuous process parameter monitoring is a quality management requirement — the LCD display provides the real-time data visibility needed to verify that the RV-50A is operating within specified process parameters throughout each batch, supporting batch record documentation and deviation detection in pharmaceutical production support and industrial chemical processing environments.
The RV-50A's PTFE and Teflon coating sealing system provides the chemical resistance required for continuous large-scale processing of organic solvents and chemical reagents. At 50L scale, seal integrity directly impacts vacuum performance and, consequently, evaporation efficiency — a compromised seal in a 50L system results in a proportionally larger vacuum leak that reduces the achieved vacuum level, extends batch processing time, and risks incomplete solvent recovery from high-value large-volume batches. The PTFE sealing specification of the RV-50A ensures durable, long-term vacuum integrity under continuous production-scale use.
The RV-50A is built on a heavy-duty aluminum alloy bracket engineered to support the considerable combined weight of a fully loaded 50L rotary flask assembly — including glassware, solvent, and the 1.75 m² condenser system. The structural design provides the rigidity, load distribution, and vibration resistance required for stable 50L-scale rotary evaporation — where the greater mechanical forces generated by rotating a large, heavy flask assembly must be safely managed to prevent structural fatigue, misalignment, and the potential for glassware failure during extended production-scale operations.
The RV-50A Rotary Evaporator integrates four independent safety systems scaled to its 5300W, 50L production-scale specification — providing critical over-current, over-temperature, power interruption, and anti-dry protection during high-volume, high-value industrial chemical and pharmaceutical solvent processing operations.
The RV-50A's 5300W rated power makes robust over-current protection an essential safety requirement. The over-current protection circuit monitors electrical current draw across the heating element and motor systems and disconnects power if current exceeds safe operating limits — protecting the heating elements, motor drive components, and laboratory electrical infrastructure from damage caused by electrical faults or component failures at this high-power operating level. In a production-scale instrument where equipment downtime has significant operational and financial consequences, over-current protection also serves as an important instrument longevity measure.
The RV-50A's independent over-temperature protection system monitors bath temperature and cuts heating power automatically if the temperature exceeds the safe upper limit — independently of the PID controller. At 50L scale with 5300W heating power, an over-temperature event has proportionally greater consequences than in smaller-scale units — generating larger quantities of excess solvent vapour, exposing greater volumes of material to thermal damage, and creating greater fire risk from the larger surface area of heated solvent. The independent protection circuit operates even if the primary PID system fails, providing essential backup protection for large-scale operations.
The RV-50A automatically restores its pre-interruption temperature setpoint and rotation speed when mains power is restored after an interruption. At production scale, an unplanned power interruption followed by incorrect restart state could require discarding a large-volume batch that has been partially processed but cannot be returned to the correct processing condition — representing significant material cost and production schedule impact. Power interruption protection eliminates this risk, maintaining batch process continuity and protecting the value of large-volume solvent processing operations running in industrial and pharmaceutical production support environments.
The RV-50A's anti-dry protection monitors the water level in its large Ø552 × 320 mm bath and activates protective shutdown if the level drops below the minimum safe threshold. At 5300W heating power, the consequences of a dry bath event are severe — heating element damage, bath material degradation, and potential fire risk from overheated dry surfaces. The larger bath volume of the RV-50A also means that greater amounts of water evaporate during extended processing sessions, increasing the frequency and importance of water level monitoring. The anti-dry protection system provides automatic, continuous monitoring that removes reliance on manual water level checks during unattended large-scale evaporation operations.
Explore alternative models and related solutions from other categories